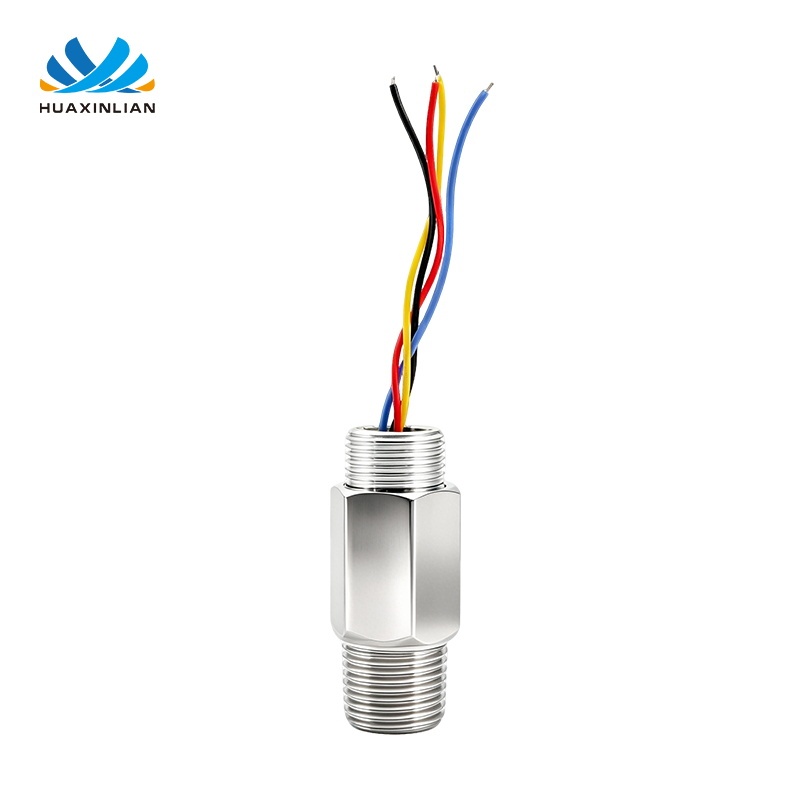
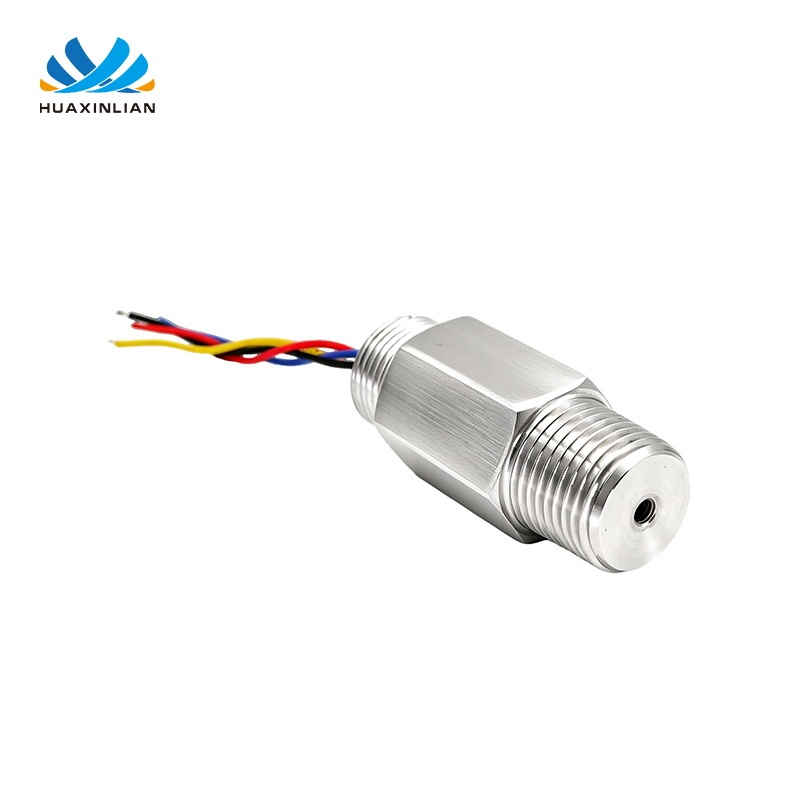
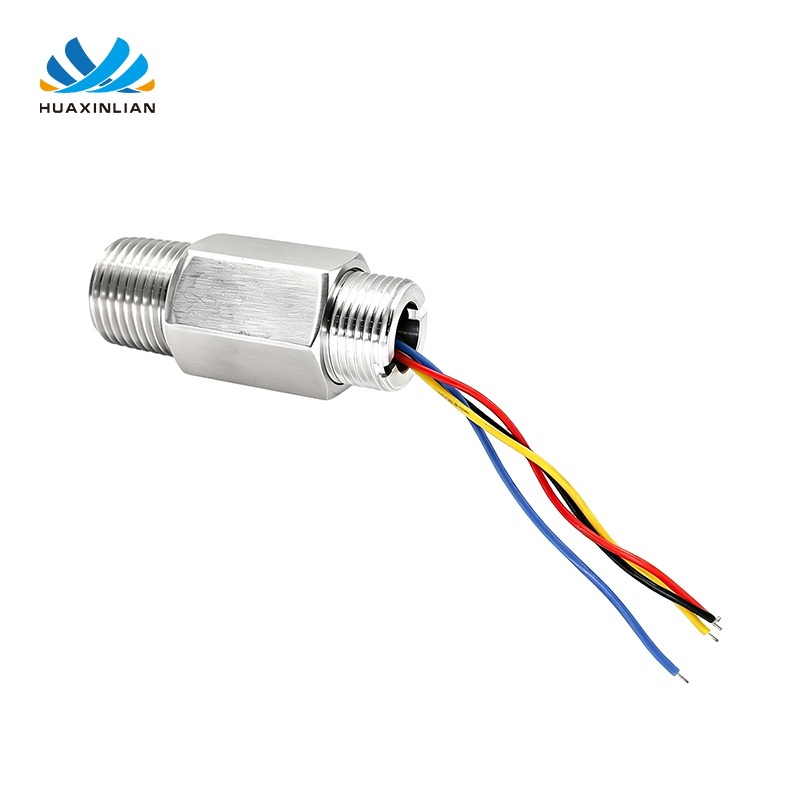
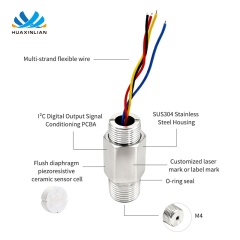
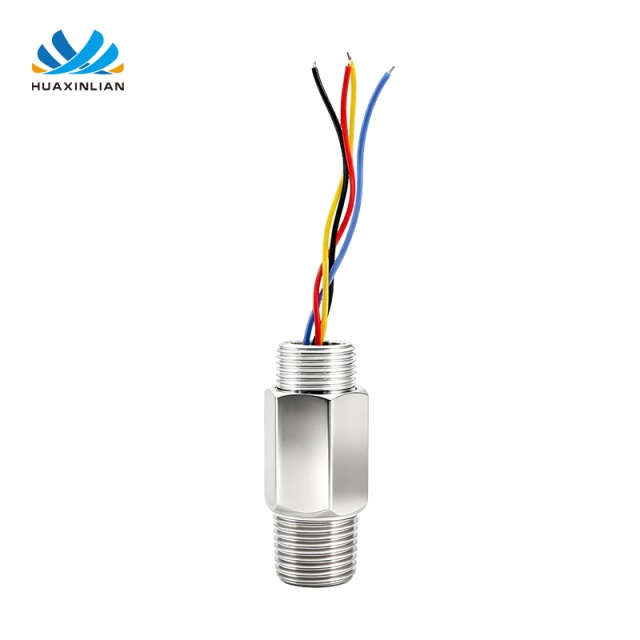
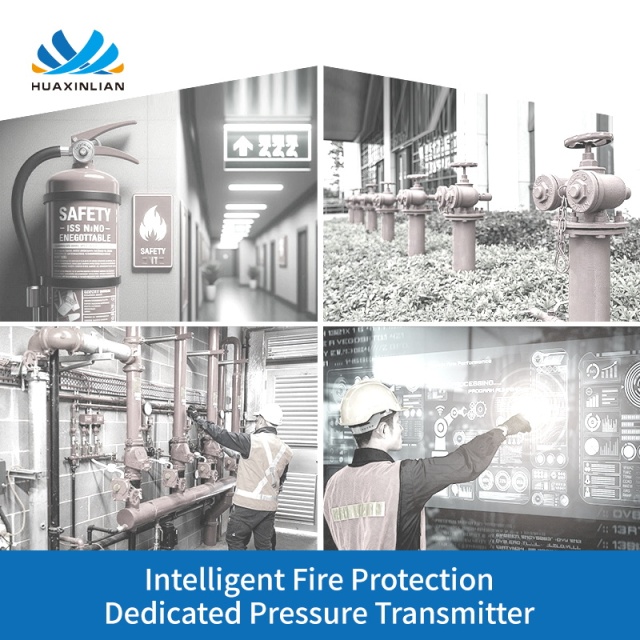
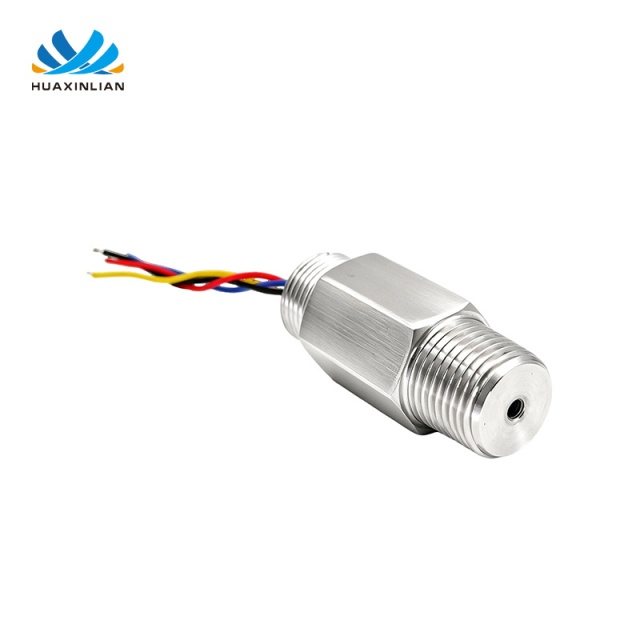
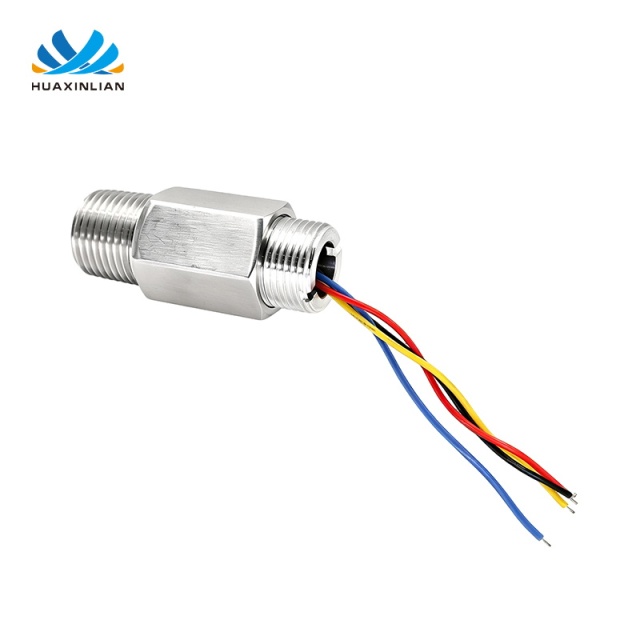
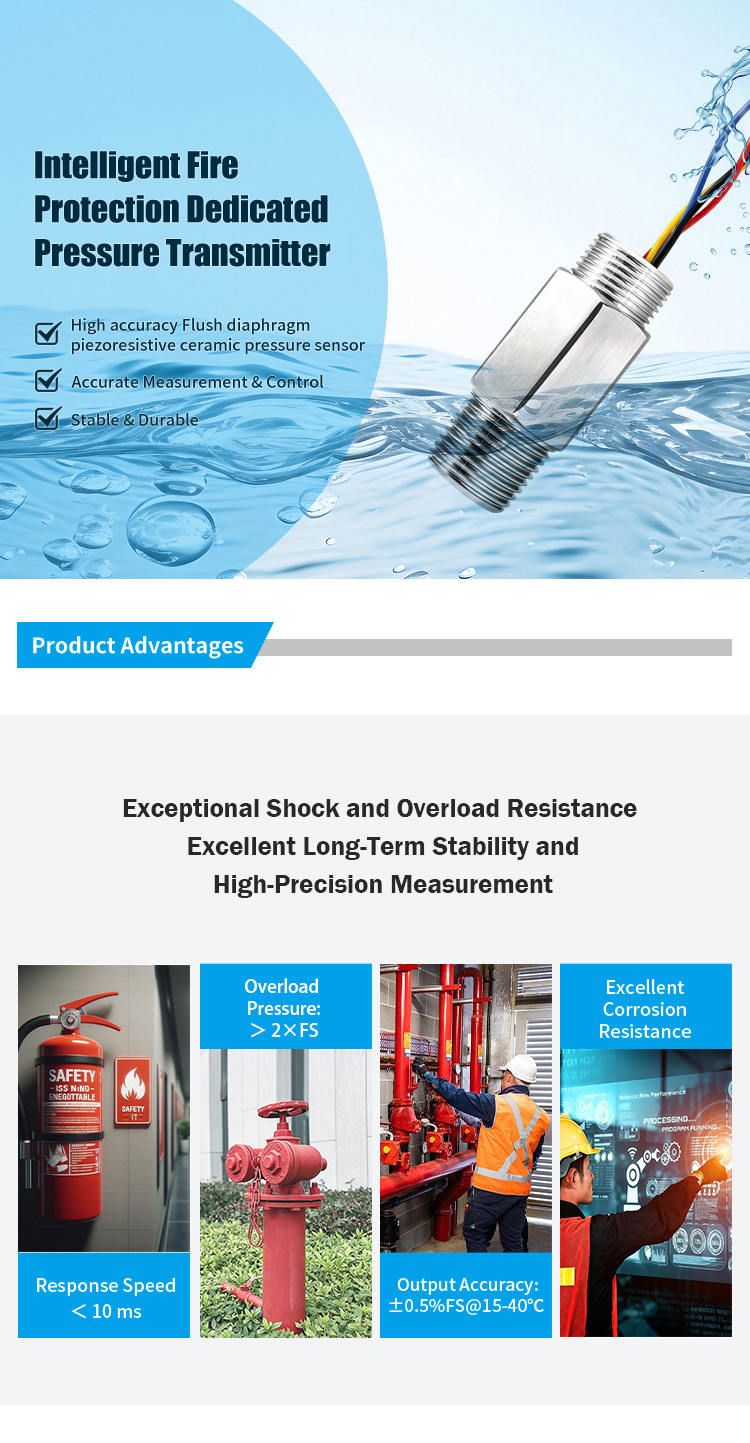
The HXL-500 pressure transmitter is expressly engineered for fire protection systems requiring precise and reliable pressure monitoring. Its ability to monitor both static and dynamic pressures allows fire safety engineers and system integrators to ensure real-time data accuracy critical for early detection and system readiness. As a specialized pressure transducer designed for harsh environments, it serves fire protection equipment manufacturers, facility managers, and safety compliance personnel needing continuous, reliable pressure feedback. This solution integrates seamlessly within fire suppression networks to uphold standards and optimize preventative maintenance cycles using advanced pressure sensor modules.
Technical Design and Measurement Capabilities
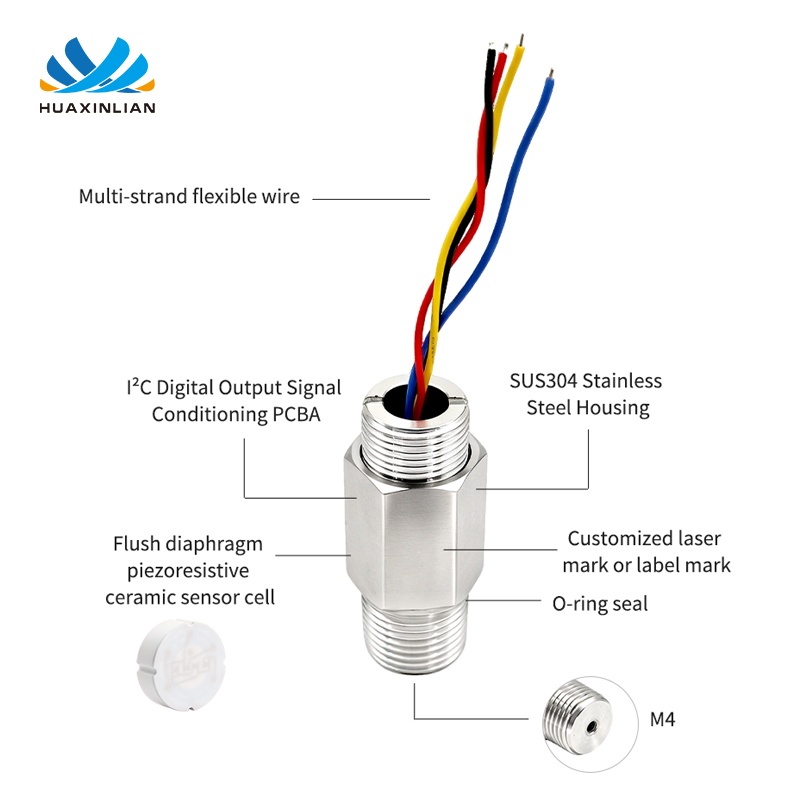
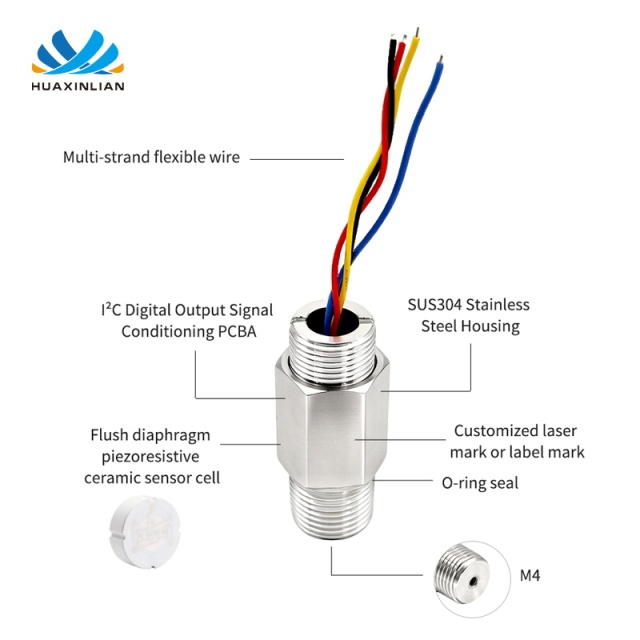
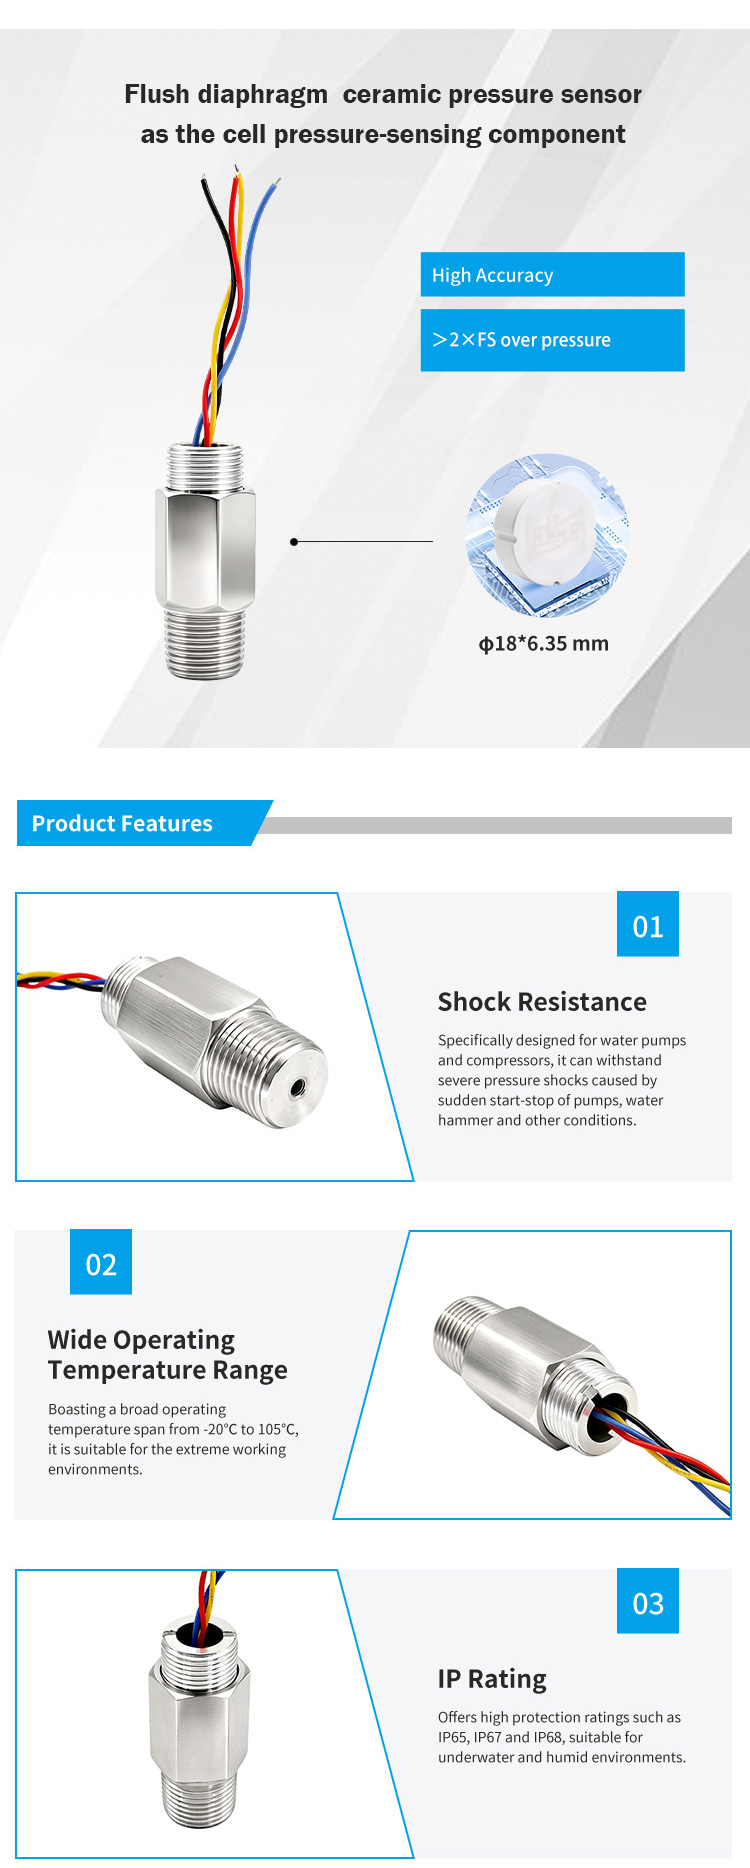
At its core, the HXL-500 utilizes a self-developed flush diaphragm ceramic sensor optimized for durability and accuracy. It incorporates comprehensive temperature compensation, including linearity correction and zero-point calibration, to maintain consistent performance across a wide operational temperature range (-40°C to 125°C). The pressure transmitter manufacturer embedded a water hammer-resistant design, providing up to five times the burst pressure capacity versus traditional piezoresistive sensors, reducing maintenance risks associated with diaphragm rupture. This pressure transducer manufacturer prioritizes stable signal output and strong anti-interference capabilities, making it suitable for integration into complex fire safety control systems requiring precise pressure sensor modules.
Practical Industry Integration and Operational Value
This intelligent pressure transmitter is integral to fire safety infrastructure across industrial and commercial sectors. It delivers high-fidelity pressure data for pipeline monitoring, enabling early anomaly detection and automatic trigger functions within fire alarm and suppression systems. Its IP68 rating ensures dependable operation even in moisture-rich, dusty, or extreme temperature conditions common in firefighting environments. The HXL-500 supports system integrators and facility operators by enhancing operational reliability and reducing downtime risks. By replacing conventional pressure transducers with this advanced ceramic pressure sensor technology, organizations achieve improved compliance with fire safety regulations and maximize the functional lifespan of critical fire protection equipment.
* Temperature resistance: -40℃ ~ 125℃
* Features a high protection rating, enabling long-term stable operation in humid and complex electromagnetic environments
* Integrates temperature measurement functionality, allowing synchronous monitoring of medium temperature
Innovative Structural Design and System Adaptability
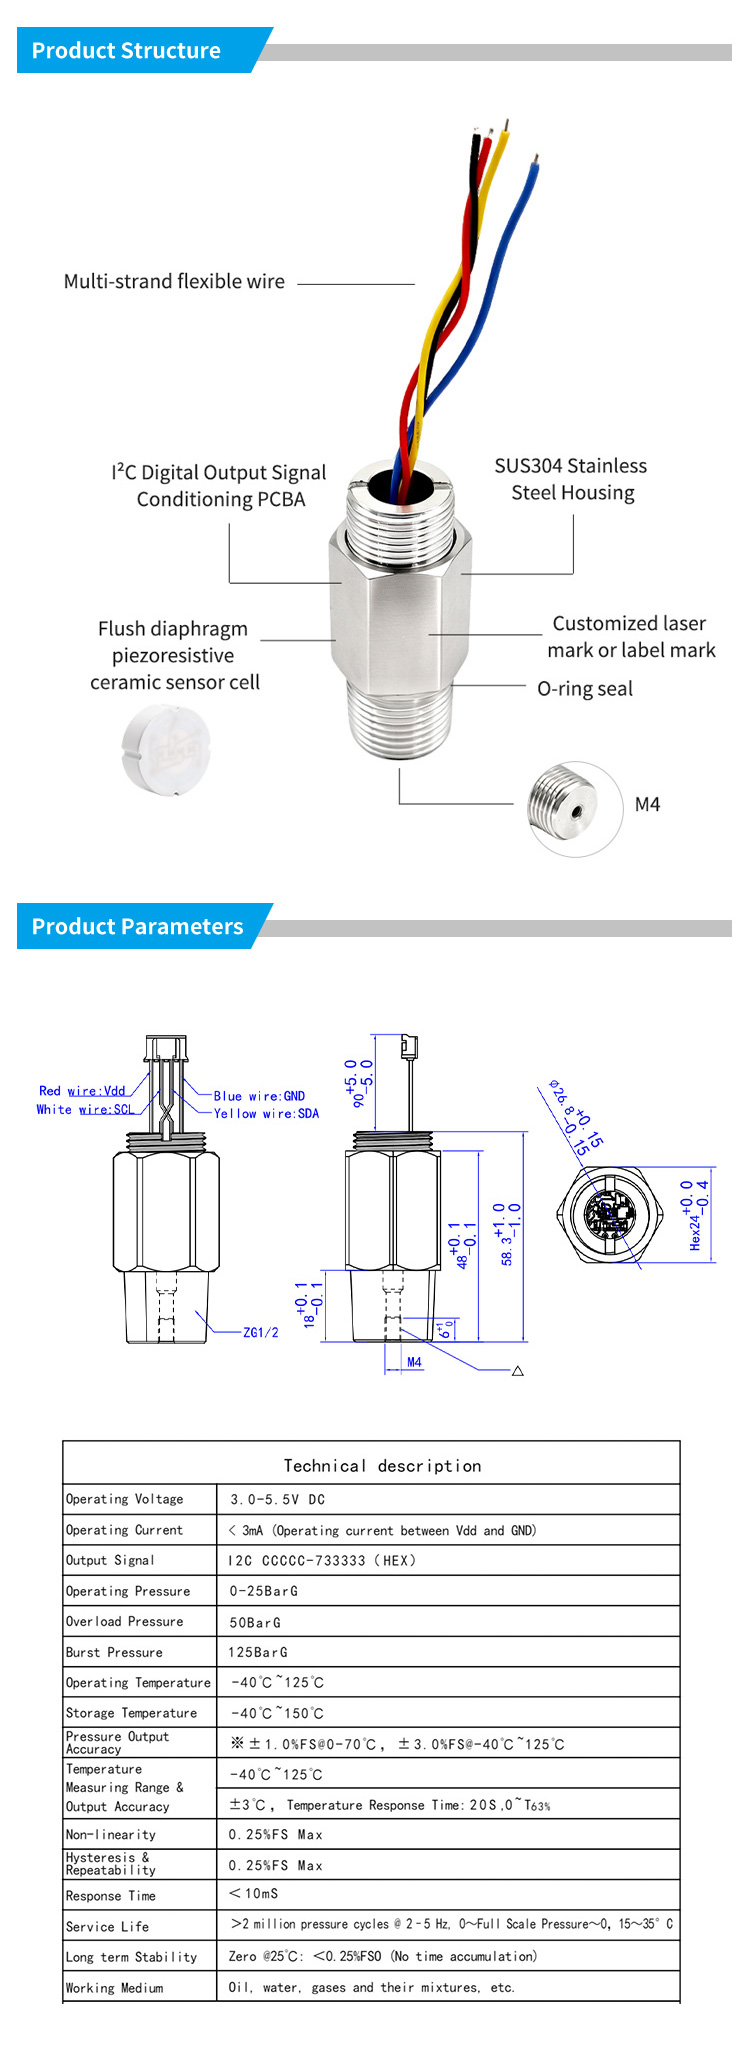
The HXL-500 features an advanced flush diaphragm ceramic sensor that eliminates common failure modes associated with traditional piezoresistive sensors. Its robust water hammer-resistant housing and IP68 ingress protection ensure durability against harsh conditions in fire protection scenarios. The modular design facilitates straightforward integration with existing pipe networks and control systems, supporting dual pressure monitoring functionalities. This pressure transmitter manufacturer emphasizes a compact yet rugged construction, allowing installation flexibility in confined spaces while maintaining structural integrity. Such features enable pressure transmitter suppliers to offer versatile, scalable solutions that cater to diverse fire protection requirements without compromising sensor reliability and accuracy.
Enhanced Performance and Operational Efficiency for End Users
Designed to deliver stable, interference-resistant signals, the HXL-500 ensures accurate real-time pressure measurement essential for critical safety systems. Built-in digital temperature compensation and calibration capabilities obviate frequent manual recalibrations, reducing operational workloads for maintenance teams. The broad temperature range compatibility and dust/water resistance extend the usable life of the pressure sensor modules in extreme environments. By providing consistent data integrity under dynamic pressure fluctuations, this pressure transducer contributes significant value to facility managers and engineers. The reliable monitoring reduces false alarms and system failures, enabling optimized resource allocation and improved compliance with safety standards.
Use Scenarios
Fire Protection Pipeline Monitoring for Automated Safety Control
In fire protection pipeline systems, the HXL-500 pressure transmitter functions as a critical monitoring node to ensure the readiness and integrity of fire suppression networks. Operating within industrial facilities and commercial buildings, it captures both static and dynamic pressure data in real-time, enabling early anomaly detection. Its robust structure and IP68 rating allow fault-free operation amidst dust, water, and temperature extremes encountered during emergencies. The pressure transducer manufacturer equips the device with advanced anti-interference design to maintain signal accuracy during transient events such as water hammer effects. This enables seamless integration with fire alarm systems, providing actionable data for automated safety responses and system diagnostics.
Quality Control and Maintenance in Firefighting Equipment Manufacturing
In firefighting equipment production environments, the HXL-500 serves as a quality assurance instrument for pressure system validation. It enables production engineers and quality managers to verify pressure thresholds and sensor responses within manufacturing lines and test benches. The ceramic pressure sensor’s resilience to harsh manufacturing conditions and its precise flush diaphragm sensor technology provide dependable, repeatable measurements. Its design supports integration into pressure sensor modules used for automated calibration and monitoring setups, enhancing throughput and reducing manual inspection errors. This application underscores the device’s role as a reliable component for pressure transducer manufacturers focused on delivering high-performance sensors tailored to fire safety equipment compliance and durability.