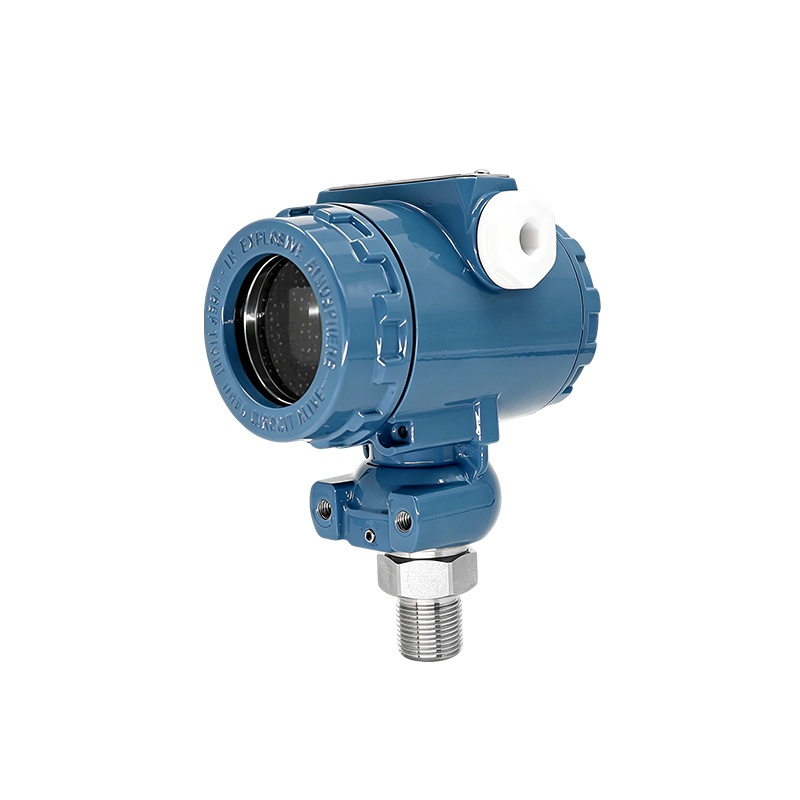
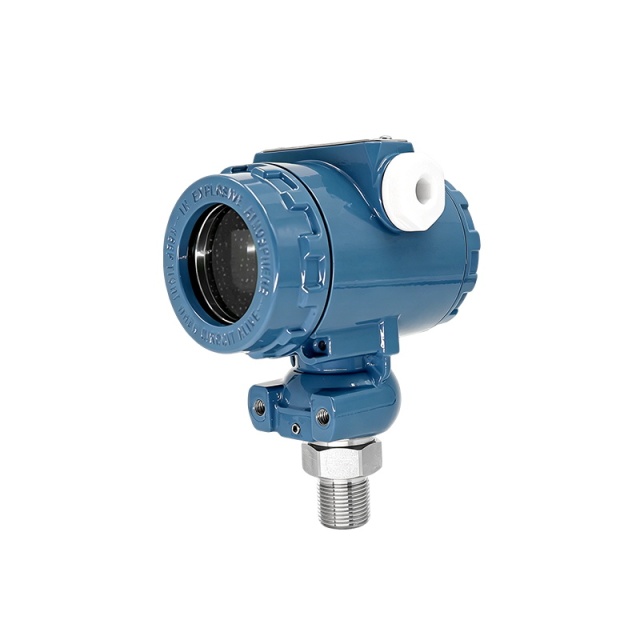
The HXL-100F pressure transmitter is engineered for industrial users requiring reliable hydraulic and pneumatic pressure measurement solutions. Designed by a leading pressure transmitter manufacturer, it supports system integrators and engineers focused on durability and accuracy in demanding environments. Its compatibility with diverse pressure ranges and thread specifications meets the customization needs of equipment in pipelines, compressors, and fluid control systems. This device enables seamless integration into existing instrumentation setups, addressing challenges faced by producers and maintenance teams who require stable output for process control and safety monitoring with water pump pressure transmitter and pressure transducer manufacturers emphasis on consistent data acquisition.
Advanced Technical Features and Measurement Capabilities
Equipped with a flush diaphragm ceramic sensor or diffused silicon options, the HXL-100F pressure transmitter integrates robust ceramic pressure sensor modules optimized for high precision. It achieves linearity better than 0.01% with long-term stability and responds within 15 milliseconds, making it suitable for fast-acting control systems. The design allows withstanding burst pressures exceeding 10 times full scale, enhancing reliability under extreme overload conditions. Signal output options include 4~20mA and RS485 protocols compatible with two-wire or four-wire configurations. Rated for operation from -40℃ to 80℃, this pressure sensor module supports wide industrial temperature ranges with explosion-proof certification, aligning with standards required by pressure transducer manufacturers deploying sensors in hazardous environments.
Industry Applications and Operational Value across Sectors
This pressure transmitter manufacturer’s HXL-100F model is widely applicable in industrial pipeline monitoring, pneumatic pressure regulation, and hydraulic system feedback loops. Its use within compressor and aircraft pressure sensing ensures compliance with safety regulations for critical infrastructure. The product’s modular adaptability allows quick replacements or upgrades across various industrial facilities, including gas transmission networks where pressure accuracy is vital. Integration into automated control systems enhances operational efficiency by providing real-time, reliable data. The advanced pressure sensor modules deliver measurable improvements in system diagnostics and preventive maintenance, reducing downtime and supporting regulatory compliance for pressure transmitter suppliers focused on robust instrumentation solutions.
* Reverse polarity protection, transient overcurrent and overvoltage protection, compliant with EMI protection requirements
| Parameters | Electrical characteristics |
|---|---|
| Pressure type | Absolute Pressure, Gauge Pressure, Sealed Gauge Pressure |
| Pressure range | -1 ... 0 ... 1000Bar (Customizable) |
| Accuracy | ±0.5% FS; ±0.25% FS; ±0.1% FS |
| Electrical performance | Two wire system; Four wire system |
| Output signal | 4~20mA; RS485 |
| Power supply voltage | 5V DC, 12V DC, 24V DC |
| Operating temperature | -40℃~80℃ |
| Storage temperature | -40℃~120℃ |
| Electrical connections | M16×1.5 Cable Gland Port |
| Pressure connection | External thread; M20×1.5; Thread specifications can be customized according to customer requirements |
| Material quality - Housing | Aluminum alloy; Customizable |
| Material quality - Sensor | Diffused Silicon/Ceramic |
| Material quality - O-shaped sealing ring | NBR/FKM/PTFE |
| Response time | ≤15ms |
| Overload pressure | >6~1.1×FS |
| Burst pressure | >10×FS (Please specify during model selection) |
| Long term stability | <0.1% FS/year (Typical); <0.2% FS/year (Maximum) |
| Cycle life | >1 million pressure cycles @2-5Hz,0~full scale pressure~0,15~35℃ |
| Protection rating | IP65 |
| Working medium | Water, weak acid solutions, mineral oil, alcohols and other liquids and gases |
Product Advantages
Structural and Design Strengths Enhancing System Integration
The HXL-100F pressure transmitter features a metal isolation diaphragm combined with a ceramic pressure sensor or a flush diaphragm ceramic sensor, providing mechanical resilience and chemical compatibility. This structural design enhances resistance to corrosion and mechanical wear, critical for longevity in harsh industrial environments. Modular construction facilitates straightforward assembly and maintenance, allowing pressure transmitter suppliers to offer customized solutions with multiple electrical and pressure connection options. The device’s intrinsic explosion-proof design complies with GB3836.4, meeting stringent safety requirements for hazardous locations. Its configurable pressure ranges and sealing materials contribute to adaptable system integration across various media, including water and mineral oils, favored by pressure transducer manufacturers targeting diverse application needs.
Performance and User-Centric Operational Benefits
From a usability perspective, the HXL-100F offers exceptional precision with minimal drift and stable outputs over extended cycles, supporting consistent process control and monitoring. High burst pressure tolerance ensures the sensor module withstands sudden pressure surges without degradation, which enhances maintenance intervals and reduces replacement costs. The transmitter’s multiple output formats, including industry-standard 4~20mA and RS485 communication, enable easy interface with control systems, benefiting system engineers from pressure transmitter manufacturer backgrounds who prioritize interoperability. Additionally, the wide operating temperature range and fast response time improve adaptability across different operational conditions, delivering value to end users requiring reliable pressure data for safety, efficiency, and regulatory adherence.
Use Scenarios
Hydraulic Systems Pressure Monitoring in Industrial Manufacturing
In manufacturing environments utilizing fluid power systems, the HXL-100F water pump pressure transmitter functions as a critical sensor for real-time pressure monitoring within hydraulic circuits. Its robust ceramic pressure sensor ensures accuracy and durability under high-pressure surges commonly experienced in heavy machinery operations. By integrating with automation systems, the device facilitates precise pressure control necessary for maintaining machine performance and preventing system failures. Its specifications from a top-tier pressure transmitter manufacturer ensure compliance with safety standards, reducing downtime and enhancing predictive maintenance strategies within complex hydraulic networks.
Pressure Verification in Compressed Natural Gas (CNG) Pipelines
For gas transmission infrastructure, pressure transmitter suppliers recommend the HXL-100F due to its intrinsic explosion-proof certification and high burst pressure resistance. It plays a vital role in continuous pressure verification and leak detection in CNG pipelines, where safety and regulatory compliance are paramount. The transmitter’s ability to perform accurate, stable measurements across wide temperature ranges under hazardous conditions ensures system reliability. It seamlessly integrates with industrial control platforms to provide operators immediate status updates, facilitating prompt corrective actions. The flush diaphragm ceramic sensor design reduces sensor fouling and degradation by resistant media, enhancing long-term operational integrity in gas transport environments.